Applications / By industry, material & process

Start with the part.

From aerospace brackets to lamp molds — start from the geometry, material and tolerance of your part, and we'll point to the platform and process that fit.

What we machine.

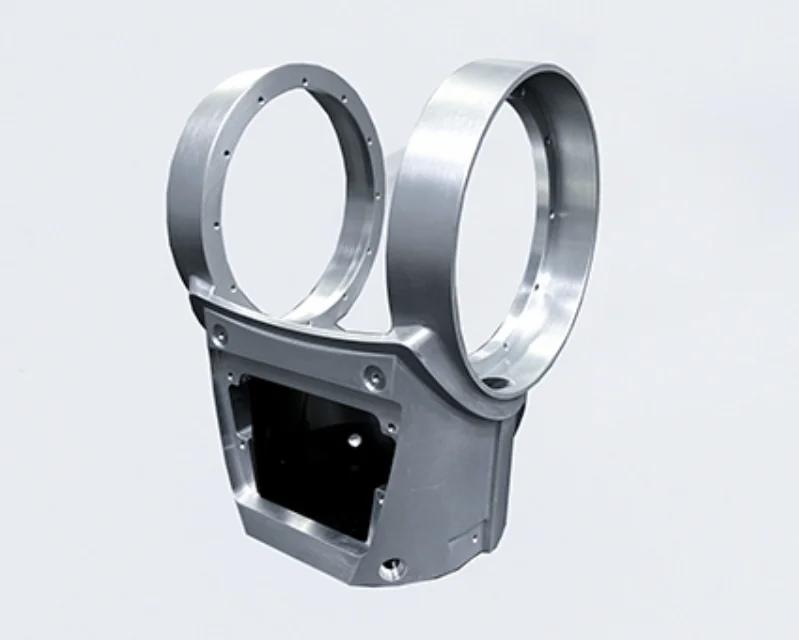
Five-axis machined aluminium aerospace bracket with two large bores

Aerospace

Compact aluminium fittings one week, large titanium impellers the next. Five-face machining on the G300 and heavy contouring on the cradle-type U series cover both ends of the mix.

Parts — Structural brackets / Impellers & blisks / Actuator housings

Materials — 7075 aluminium · Titanium · Alloy steel

Platforms — G300 · G630 / G800 · U1000

Explore Aerospace
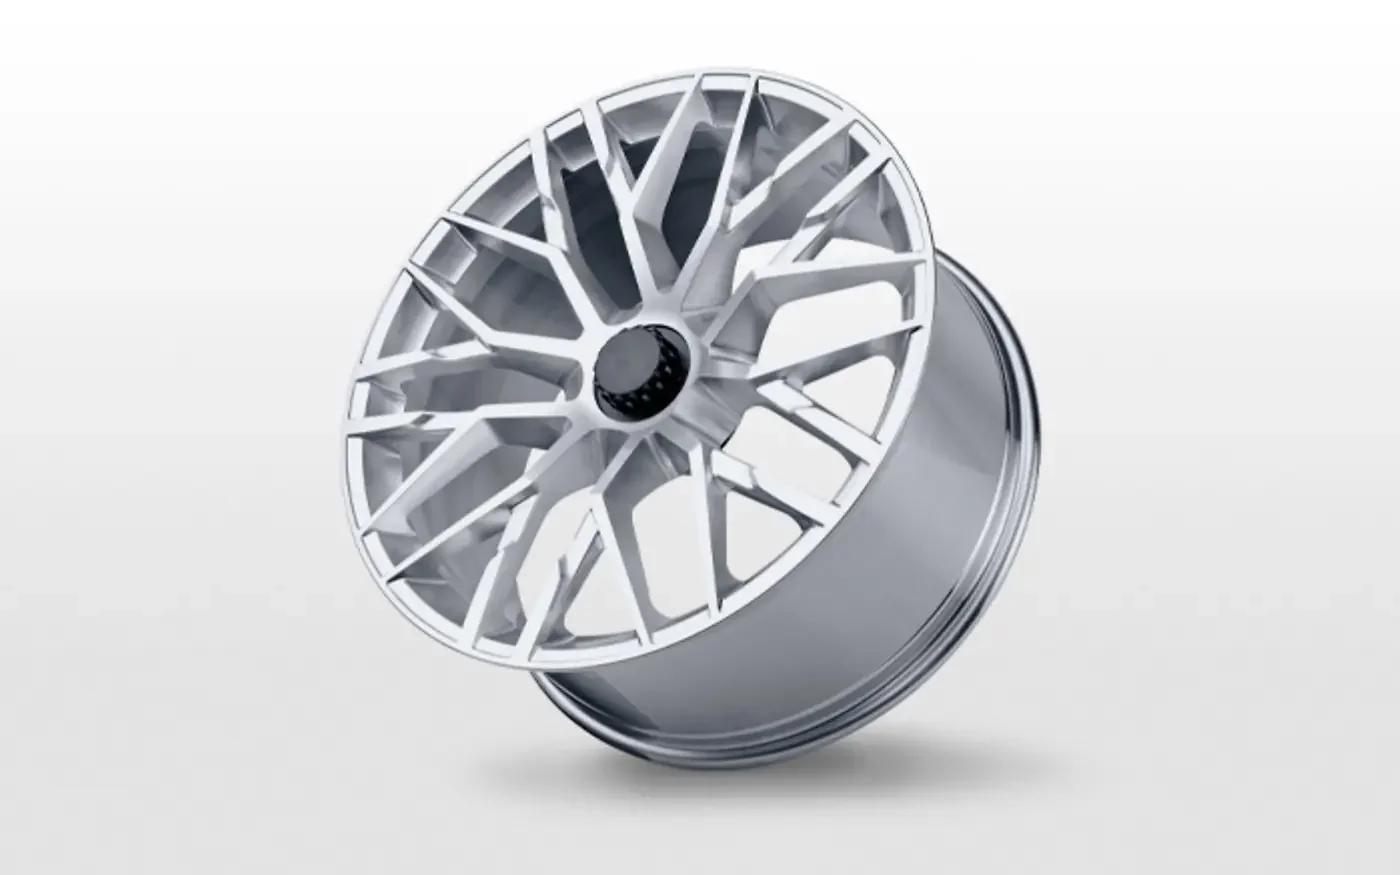
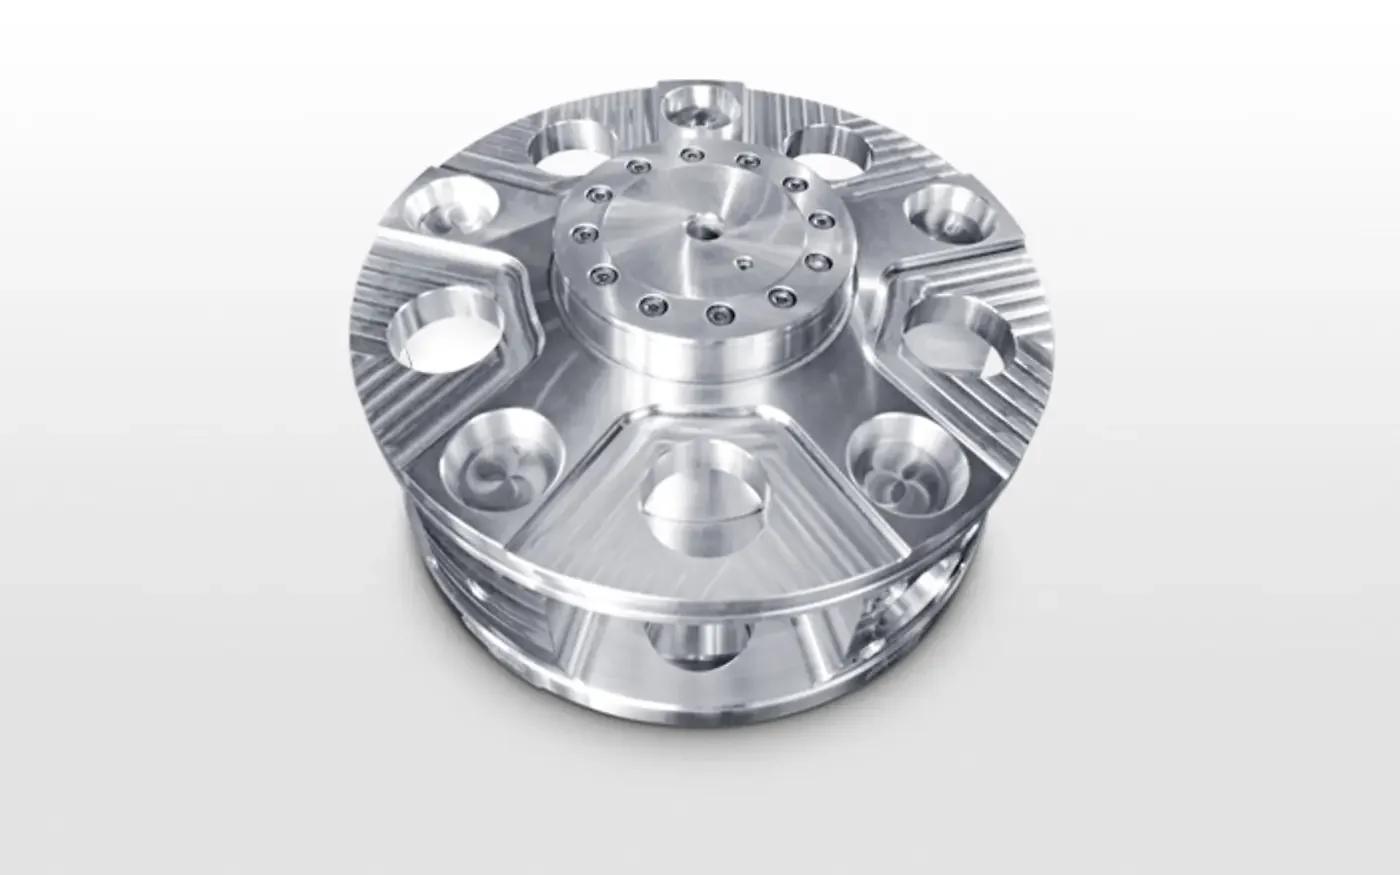
Machined wheel hub with radial spokes and a central bore

Automotive

Hubs and engine blocks in steel and cast iron, housings and covers in aluminium. Multi-station hydraulic fixturing keeps several parts clamped per cycle.

Parts — Wheel hubs / Engine blocks / Gearbox housings

Materials — Carbon steel · Grey cast iron · Aluminium

Platforms — G630 / G800 · U Series

Explore Automotive
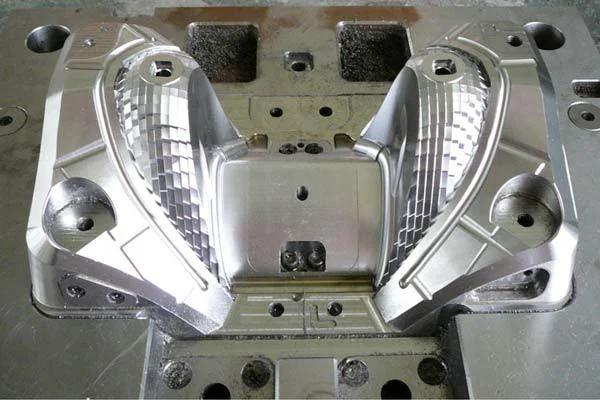
Pair of polished headlamp reflector mold cavities

Mold & Die

Lamp reflectors, mold cores and die-casting tools — free-form surfaces from R3 to R300 mm finished in one cradle setup, without a hand-polish step.

Parts — Lamp molds / Mold cores / Die-casting dies

Materials — Hardened mold steel · Aluminium · Copper

Platforms — U1000 · U Series

Explore Mold & Die
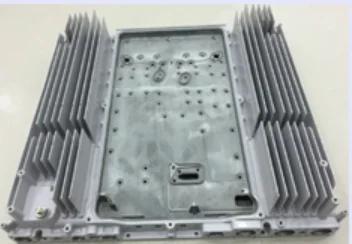
Die-cast filter housing with deep cavities and narrow ribs

5G & Telecom

Large filter cavities are deep and feature-dense. Cradle-type five-axis machining opens cavities, narrow slots and threads in a single setup.

Parts — Filter cavities / Heat-sink plates / RF housings

Materials — Die-cast aluminium

Platforms — U1250 · U1600 · U Series

Explore 5G & Telecom
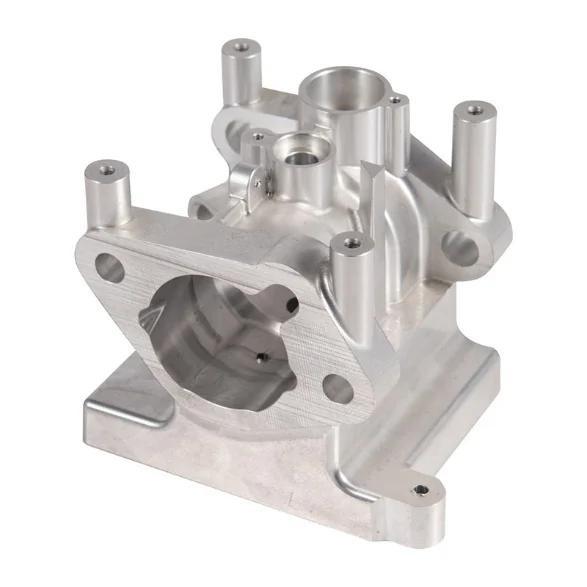
Complex machined aluminium robot component with internal cavities

Robotics

Die-cast aluminium joints and housings with threads, bores and tapped holes in the same part — five faces in two operations on the G300.

Parts — Robot joints / Die-cast housings / Sensor mounts

Materials — Die-cast aluminium

Platforms — G300

Explore Robotics
Machined planet carrier with a ring of bores on a flange

Precision Components

Planet carriers, frames and ring parts, run in small batches — where straightness over the full length and concentricity decide the process.

Parts — Planet carriers / Frame structures / Disc & ring parts

Materials — Alloy steel · Cast iron · 7075 aluminium

Platforms — G630 / G800 · U1250

Explore Precision Components

Materials we machine.

6061 Aluminium

Structural parts and housings; high-speed finishing keeps thin walls stable.

G300

7075 Aluminium

High-strength aerospace parts; chip control and tool life need attention.

G300 · G630 / G800

Die-cast Aluminium

Robot and housing parts; roughing to finishing on one platform.

G300 · U Series

Carbon Steel

Hubs and heavy blanks; rigid setups keep heavy roughing predictable.

G630 / G800

Grey Cast Iron

Engine blocks and carriers; stable cuts with predictable tool wear.

G630 / G800

Alloy Steel

Impellers, hubs and planet carriers.

G630 / G800 · U1000

Titanium (TC4)

Impellers and structural parts; high-pressure coolant and controlled cutting forces.

U1000 · G630 / G800

03 / Processes & geometry

The geometry decides the process.

Every part below was cut on a DEPU five-axis platform — these are the recurring problems the processes were built around.

01

Five faces, fewer setups

One datum face, then five faces without moving the part — no stacked error from re-clamping.

02

Deep cavities, long overhangs

Vibration-damped boring holds 8:1 length-to-diameter bores inside deep cavities.

03

Mirror finishes on free-form surfaces

Fast point milling holds reflector-class surfaces without a hand-polish step.

04

Thin walls, high-speed finishing

Light, fast passes keep thin ribs and frames stable.

05

Deep ribs and narrow slots

Trochoidal roughing with radial-depth control; taper compensation for slot walls.
Reference cases.

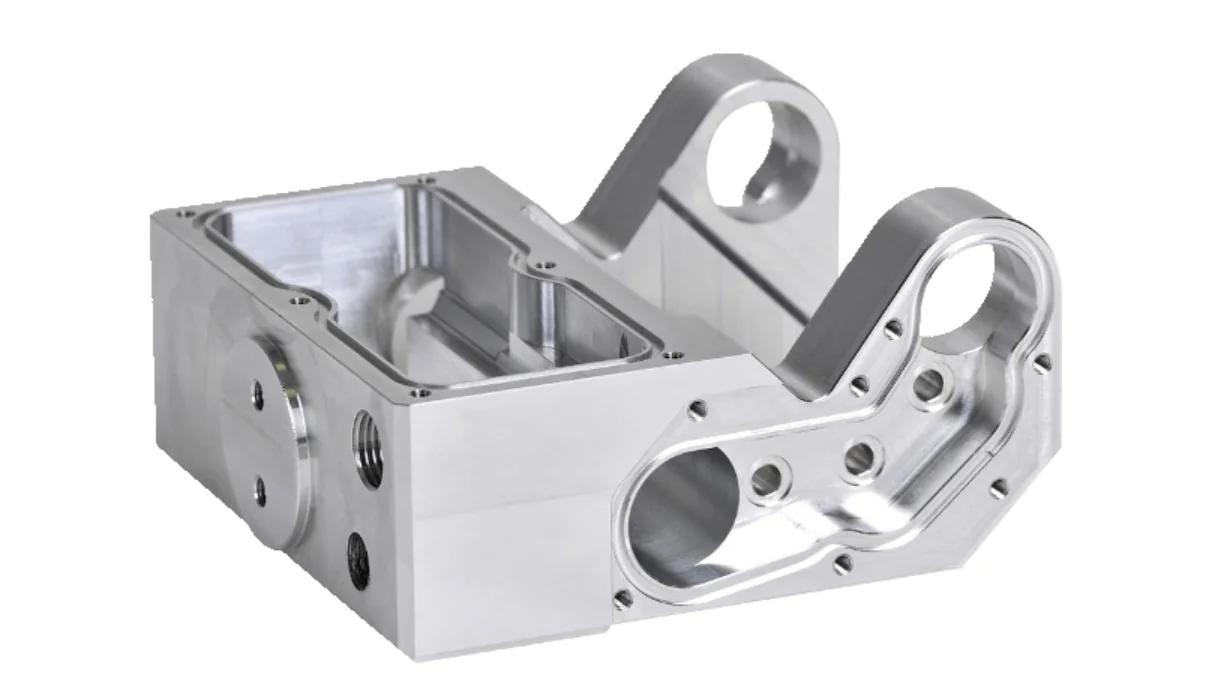
G300 application reference part after five-face machining

Machines — G300
Material — 7075 aluminium
Part — 198 × 185 × 88.5 mm

Case 01

Aerospace structural parts on the G300

Square billets machined to five faces in two operations, with deep holes, bores and threads in the same part.

A precision parts maker running high-mix orders across aerospace, robotics and industrial equipment.

Challenge

  • Five-face parts required several machines; stacked error decided the assembly fit.
  • Deep holes at an 8:1 ratio had a tendency to drift.
  • Thin aluminium walls were unstable at high feed rates.

Approach

  • OP01 machines the datum face; OP02 reaches the remaining five faces.
  • HSK-E50 spindle at up to 24,000 rpm for high-speed aluminium cutting.
  • Internal threads, bored bores and deep holes completed on one fixture.
±0.02 mmSurface accuracy
Ra ≤ 0.8 µmSurface roughness
32 minPart cycle time
Machined wheel hub from the G630 / G800 application reference

Machines — G630 / G800
Material — Carbon steel · Cast iron · Titanium
Part — Wheel hubs · Engine blocks · Impellers

Case 02

Heavy parts on the G630 / G800

Wheel hubs, engine blocks and impellers on one platform — steel, cast iron, aluminium and titanium.

A heavy-equipment manufacturer building parts for NEV and aerospace programmes.

Challenge

  • Engine blocks needed several separate clampings, accumulating positioning error.
  • Titanium impellers were slow to cut and hard on tooling.
  • Changeover for carriers and frames ran to hours.

Approach

  • One-clamping machining for engine-block assemblies.
  • Heavy roughing on the G800 with a high-torque spindle.
  • Five-axis simultaneous finishing of impeller flow passages.
18 minWheel-hub cycle
±0.015 mmImpeller accuracy
Ra 0.4 µmImpeller finish
Headlamp reflector mold cavities after five-axis finishing

Machines — U1000
Material — Hardened mold steel · Aluminium
Part — Lamp reflectors · Filter cavities

Case 03

Lamp molds and impellers on the U1000

Reflector surfaces and deep filter cavities finished on a cradle table — without a hand-polish step.

A precision mold maker serving automotive lighting and 5G communications.

Challenge

  • Headlamp reflectors needed several stations, accumulating surface error.
  • Deep, narrow slots in filter cavities caused tool interference.
  • Impeller flow passages dominated the total lead time.

Approach

  • Cradle-type table: A ±120° / C 360° swings the workpiece to the tool.
  • Free-form surfaces from R3 to R300 mm machined in one setup.
  • High-speed point milling holds the reflector finish without manual polishing.
32 h → 9 hLamp-mold cycle
Ra 0.2 µmImpeller finish
A ±120° / C 360°Cradle travel

Where to start.

Structural parts · five facesG300View G300
Wheel hubsG630 / G800View G630View G800
Engine blocks & housingsG630 / G800View G630View G800
Impellers & blisksU1000 · G630 / G800View U1000View G630
Lamp molds & coresU1000 · U1250View U1000View U1250
Filter cavitiesU1250 / U1600View U1250View U1600

Bring the part. We'll bring the process.

Tell us the geometry, material and tolerance — we'll map it to a platform and a first-pass process.

Discuss your application