Case 03Read the full case
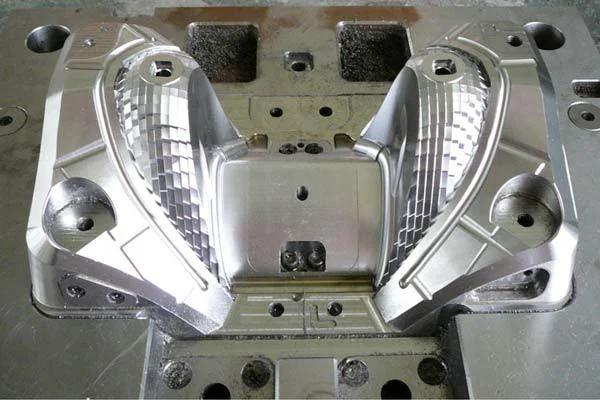
Lamp molds and impellers on the U1000
Reflector surfaces and deep filter cavities finished on a cradle table — without a hand-polish step.
32 h → 9 h
Ra 0.2 µm
A ±120° / C 360°
Five-axis applications
Lamp reflectors, mold cores and die-casting tools — free-form surfaces from R3 to R300 mm finished in one cradle setup. The high-speed point-milling process holds the surface without a hand-polish step.
Discuss your application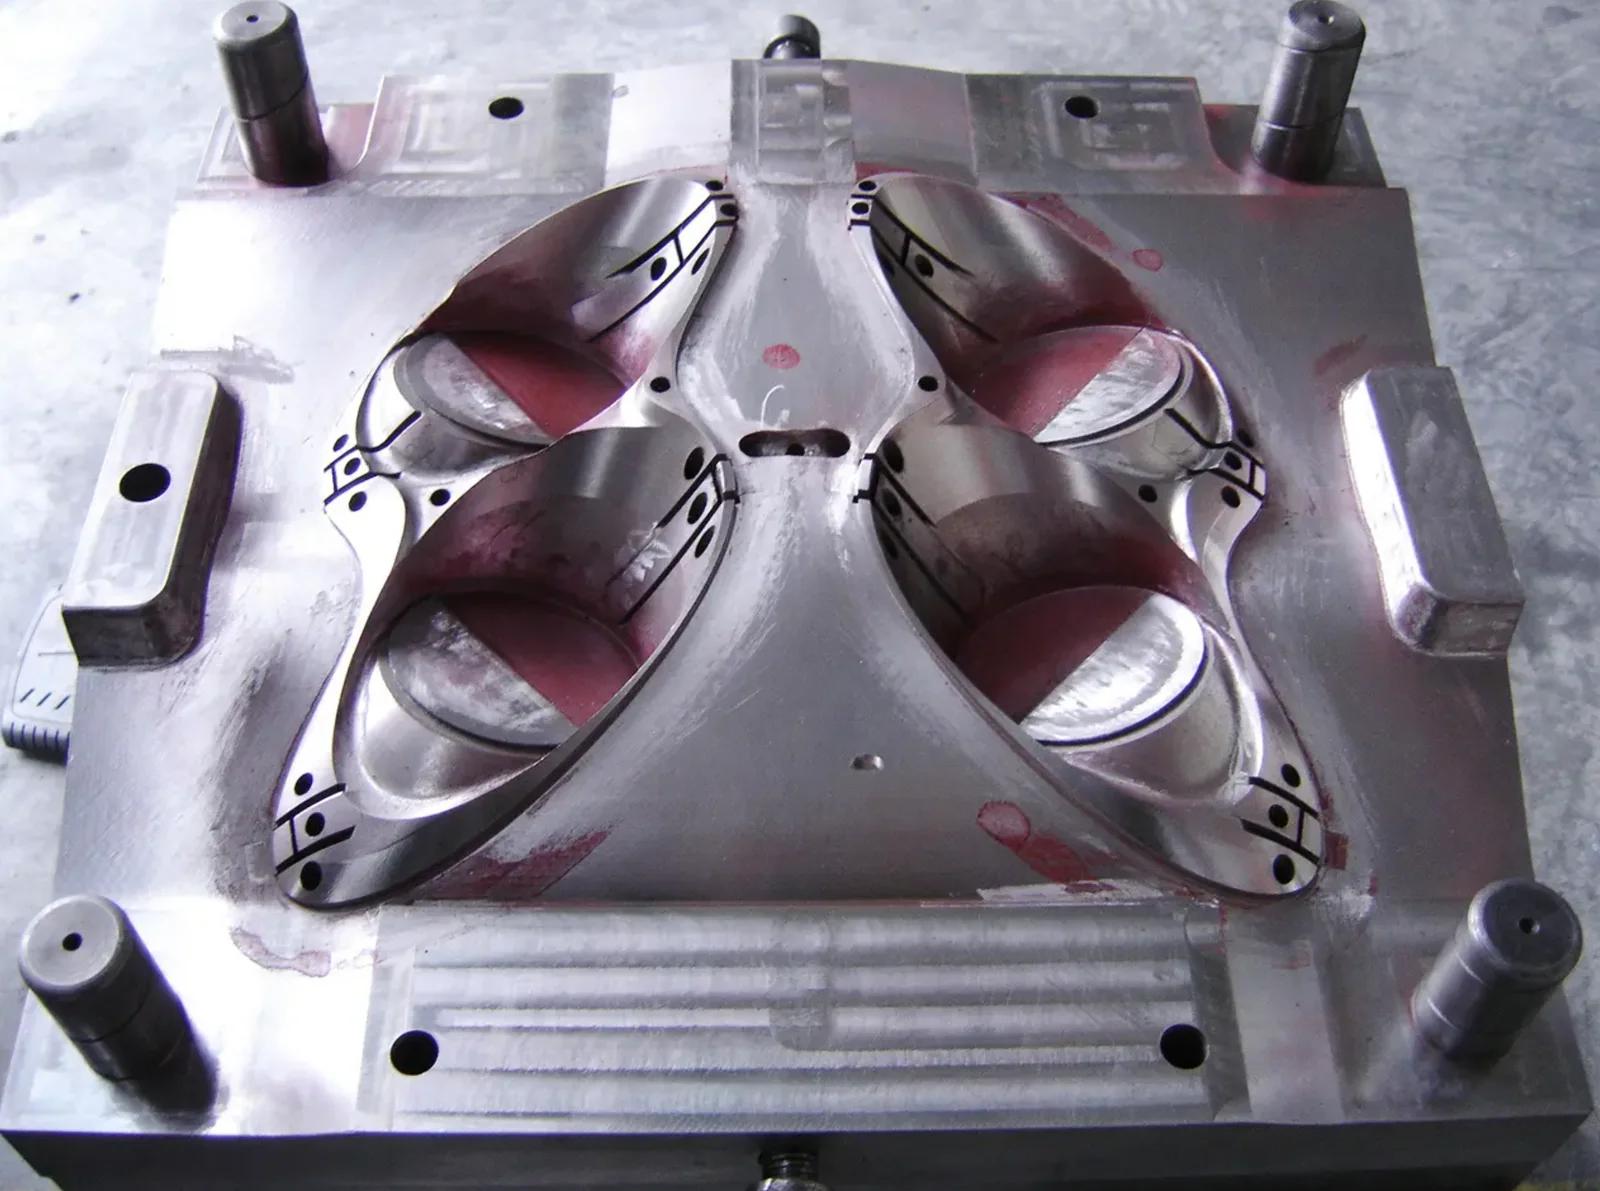
Free-form reflector surfaces with steep curvature, machined in one cradle setup.
Deep cavities and narrow slots, with taper compensation for slot walls.
Hardened mold steel, aluminium and copper electrodes on the same machine.
High-speed surface finishing of sculpted cavities.
Vibration-damped boring holds 8:1 length-to-diameter bores inside deep cavities.
Fast point milling holds reflector-class surfaces without a hand-polish step.
Trochoidal roughing with radial-depth control; taper compensation for slot walls.
Reflector surfaces and deep filter cavities finished on a cradle table — without a hand-polish step.
Tell us the geometry, material and tolerance — we'll map it to a platform and a first-pass process.
Discuss your application