Case 02Read the full case
Heavy parts on the G630 / G800
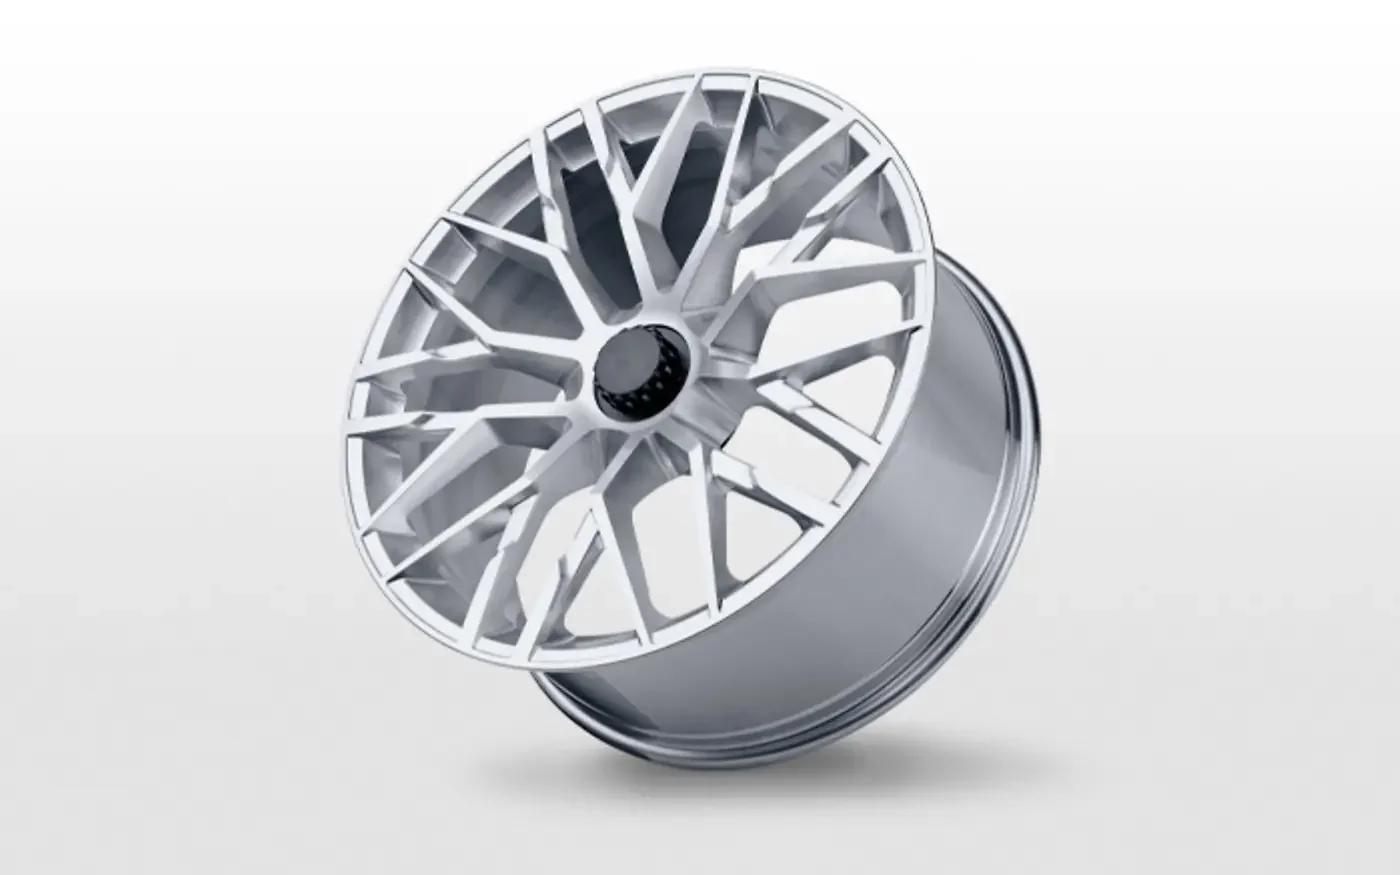
Wheel hubs, engine blocks and impellers on one platform — steel, cast iron, aluminium and titanium.
18 min
±0.015 mm
Ra 0.4 µm
Five-axis applications
Planet carriers, frames and ring parts, run in small batches — where straightness over the full length and concentricity decide the process. Multi-face castings and box bodies arrive with every face open to the tool.
Discuss your application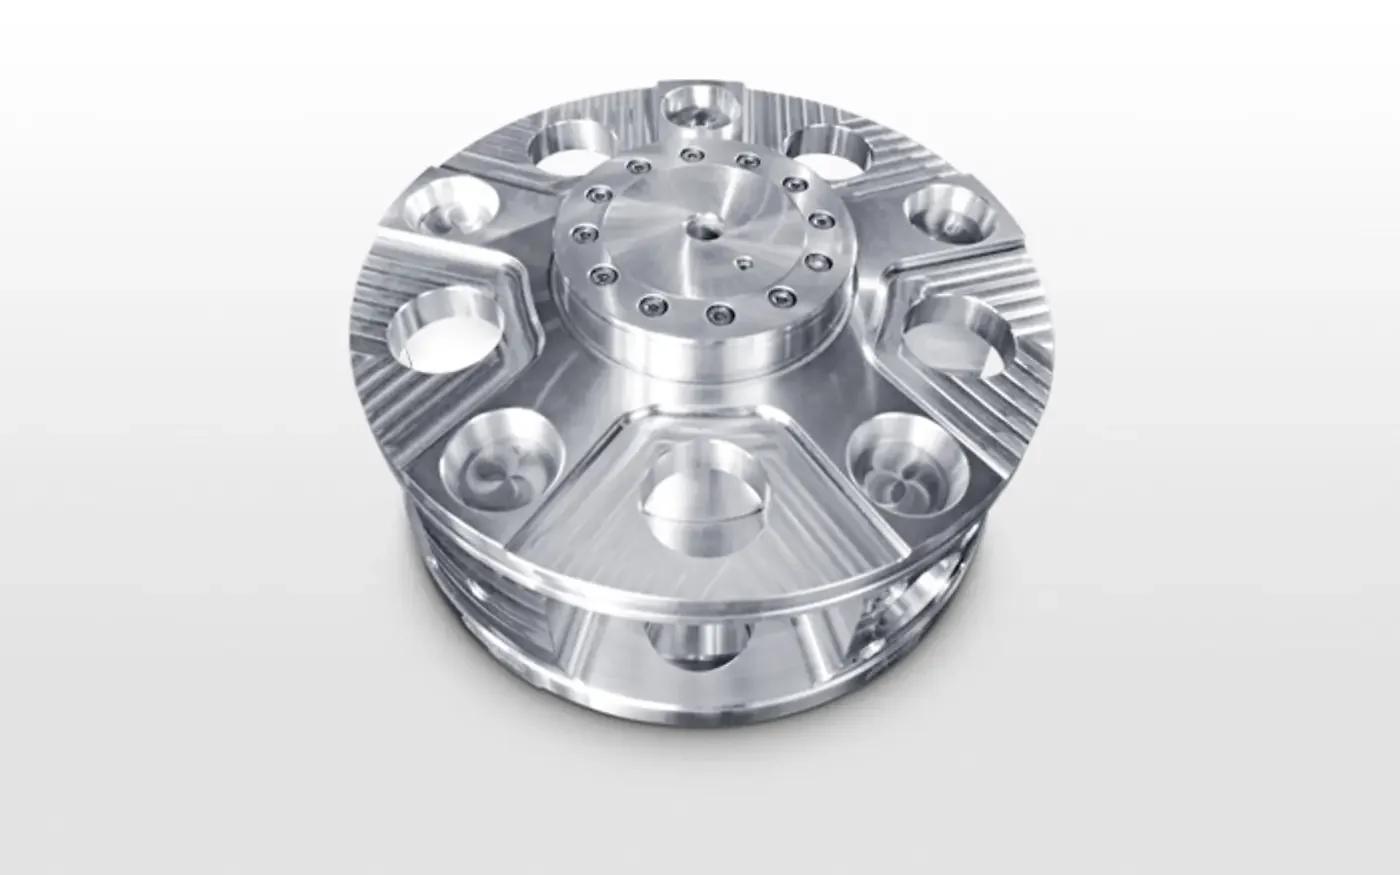
Long-overhang boring inside a deep cavity, held with a vibration-damped bar.
7075 aluminium frames with thin ribs and open pockets; straightness over the full part length decides the process.
Concentricity-driven turning and milling on one platform.
Multi-face and cylinder-block die castings completed in one clamping.
One datum face, then five faces without moving the part — no stacked error from re-clamping.
Vibration-damped boring holds 8:1 length-to-diameter bores inside deep cavities.
Light, fast passes keep thin ribs and frames stable.
Wheel hubs, engine blocks and impellers on one platform — steel, cast iron, aluminium and titanium.
Tell us the geometry, material and tolerance — we'll map it to a platform and a first-pass process.
Discuss your application