Case 01Read the full case
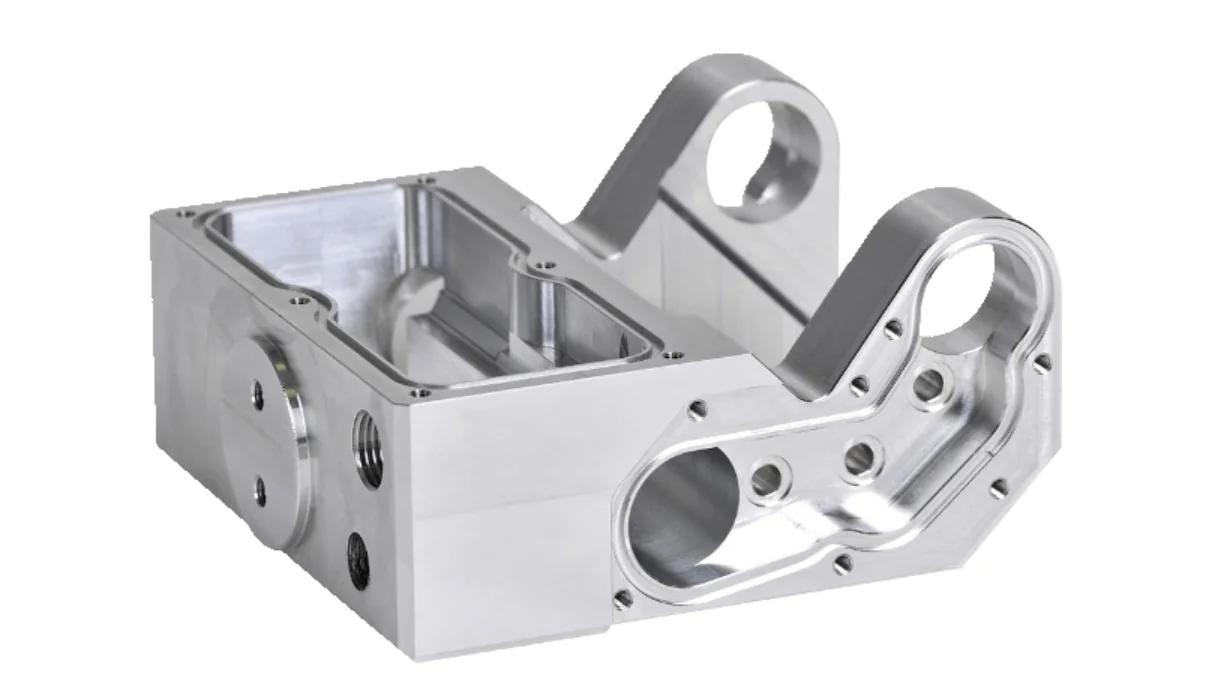
Aerospace structural parts on the G300
Square billets machined to five faces in two operations, with deep holes, bores and threads in the same part.
±0.02 mm
Ra ≤ 0.8 µm
32 min
Five-axis applications
Compact aluminium fittings one week, large titanium impellers the next. Five-face machining on the G300 and heavy contouring on the cradle-type U series cover both ends of the mix — from airframe structural parts to engine hardware.
Discuss your application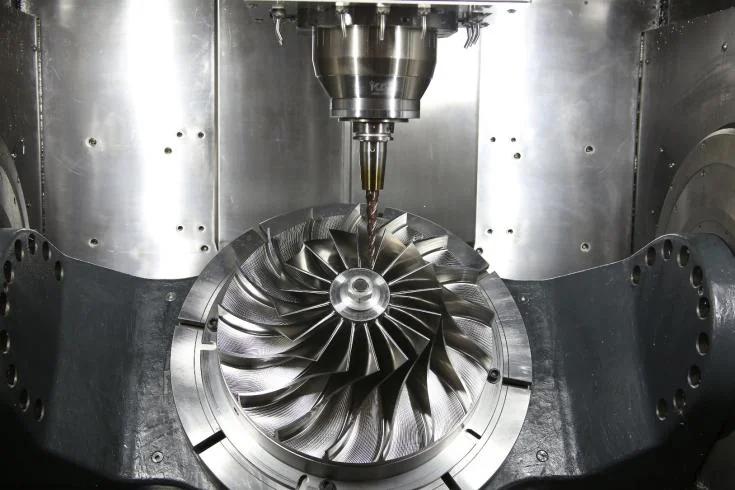
Square billets machined to five faces in two operations on the G300, with bores, threads and deep holes in the same part.
Five-axis simultaneous contouring of blade passages, in aluminium, alloy steel and titanium.
Contoured surfaces finished at high spindle speed on the tilting-head and cradle-type platforms.
Multi-face housings with internal features completed on one fixture.
One datum face, then five faces without moving the part — no stacked error from re-clamping.
Vibration-damped boring holds 8:1 length-to-diameter bores inside deep cavities.
Fast point milling holds reflector-class surfaces without a hand-polish step.
Square billets machined to five faces in two operations, with deep holes, bores and threads in the same part.
Tell us the geometry, material and tolerance — we'll map it to a platform and a first-pass process.
Discuss your application